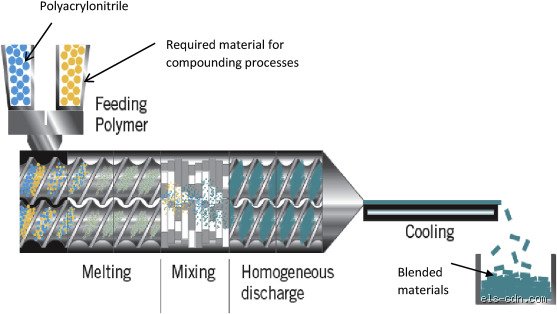
Understanding how polyacrylonitrile is fabricated requires a deep dive into polymer chemistry, reaction engineering, and complex rheological processing. Because PAN possesses unique chemical properties—chief among them being a strong intermolecular dipole-dipole attraction caused by its pendant nitrile groups—it does not melt under normal atmospheric conditions. Instead, it undergoes thermal degradation before reaching a liquid state. Consequently, standard thermoplastic shaping methods such as injection molding or melt extrusion cannot be employed. Fabricating PAN into usable fibers or films demands specialized polymerization routes and sophisticated solution-spinning technologies.
1. The fundamental chemistry and molecular architecture
To appreciate the fabrication workflow of polyacrylonitrile, one must first examine its molecular structure. PAN is a vinyl polymer formed by the addition polymerization of acrylonitrile monomers (CH2=CH−CN ext{CH}_2= ext{CH}- ext{CN}CH2=CH−CN). The resulting polymer chain consists of a carbon-carbon backbone with alternating carbon atoms bearing a strongly polar nitrile group (-C≡N ext{-C}\equiv ext{N}-C≡N).
The presence of these nitrile groups dictates virtually every physical and chemical characteristic of the polymer:
Intermolecular Forces: The high electronegativity of the nitrogen atom creates a substantial dipole moment across the nitrile group. Neighboring polymer chains exert strong dipolar attractions on one another.
Chain Stiffness and Crystallinity: These robust dipole-dipole interactions, combined with steric hindrance, restrict the rotational freedom of the polymer backbone. This results in a rigid, highly oriented structure that readily forms crystalline domains.
Thermal Behavior: Because the energy required to disrupt the intermolecular dipole network exceeds the thermal energy needed to break covalent bonds along the backbone, PAN thermally degrades (via cyclization and cross-linking) around 200°C to 300°C, well below any theoretical melting point.
Because melt-processing is impossible, fabrication must strictly rely on solution-based polymerization followed by wet or dry-jet-wet spinning processes.
2. Monomer synthesis and Purification
The fabrication journey begins upstream with the production of the monomer itself: acrylonitrile (C3H3N ext{C}_3 ext{H}_3 ext{N}C3H3N). Globally, the dominant industrial route for synthesizing acrylonitrile is the Sohio process (Standard Oil of Ohio), developed in the 1950s.
In this catalytic ammoxidation process:
Propylene (C3H6 ext{C}_3 ext{H}_6C3H6), ammonia (NH3 ext{NH}_3NH3), and oxygen (from air) are fed into a fluidized-bed reactor.
The reaction occurs at elevated temperatures (typically 400°C to 500°C) in the presence of a heterogeneous metal oxide catalyst (frequently bismuth phosphomolybdate or similar complex multi-component metallic oxides).
The overall chemical transformation proceeds as follows:
CH3CH=CH2+NH3+1.5O2→CH2=CH−CN+3H2O ext{CH}_3 ext{CH}= ext{CH}_2 + ext{NH}_3 + 1.5 ext{O}_2 ightarrow ext{CH}_2= ext{CH}- ext{CN} + 3 ext{H}_2 ext{O}CH3CH=CH2+NH3+1.5O2→CH2=CH−CN+3H2O
Following synthesis, the raw product stream undergoes rigorous fractional distillation and water scrubbing to separate unreacted gases, hydrogen cyanide (a hazardous byproduct), acetonitrile, and other impurities. High-purity acrylonitrile (typically >99.5% purity) is essential because even trace impurities can act as chain terminators or uncontrollable cross-linking agents during the subsequent polymerization phase.
3. Co-Polymerization strategies for precursor tailoring
While homopolymers of acrylonitrile can be synthesized, commercial PAN utilized for carbon fiber precursors is almost invariably a copolymer or terpolymer. Pure PAN homopolymer chains pack so tightly and rigidly that they cyclize too rapidly and exothermically during the stabilization phase of carbon fiber production, potentially causing fiber fusion or structural defects.
To modulate the thermal behavior, crystallinity, and solubility of the polymer, small percentages (typically 1% to 10%) of co-monomers are introduced during polymerization. These co-monomers generally fall into two categories:
Neutral Co-monomers: Such as methyl acrylate (C5H8O2 ext{C}_5 ext{H}_8 ext{O}_2C5H8O2), methyl methacrylate, or vinyl acetate. These break up the regular crystalline packing slightly, enhancing solubility in spinning solvents and lowering the temperature at which initial cyclization reactions begin.
Ionic Co-monomers: Such as itaconic acid, acrylic acid, or sodium methallylsulfonate. These provide pendant carboxylic or sulfonic acid groups that act as built-in thermal initiators for the cyclization process, allowing stabilization to proceed in a controlled, gradual manner at lower temperatures.
4. Polymerization techniques: Solution vs. Suspension
The conversion of liquid monomers into solid polyacrylonitrile is achieved primarily via free-radical polymerization. Industries generally utilize two distinct methodologies: solution polymerization and aqueous suspension (slurry) polymerization.
Aqueous suspension polymerization
In suspension polymerization, acrylonitrile and selected co-monomers are dispersed in water with the aid of water-soluble free-radical initiators (such as ammonium persulfate or potassium persulfate) and stabilizing agents (like polyvinyl alcohol or cellulose derivatives).
Mechanism: The polymerization occurs inside the monomer droplets suspended in the aqueous phase. As the polymer chains grow, PAN has extremely low solubility in water, causing it to precipitate out as fine white powder particles (slurry).
Advantages: This method allows for high reaction yields, excellent heat dissipation (as water acts as an efficient thermal sink), and straightforward separation of the polymer powder via filtration or centrifugation.
Disadvantages: The resulting polymer powder must subsequently be washed, dried, and dissolved into an appropriate organic or inorganic solvent before fiber spinning can commence.
Solution Polymerization
In solution polymerization, monomers, initiators, and co-monomers are dissolved directly into a specialized solvent in which both the starting materials and the resulting PAN are soluble. Common solvents include polar organic liquids like dimethylformamide (DMF), dimethyl sulfoxide (DMSO), dimethylacetamide (DMAc), or concentrated aqueous inorganic solutions like zinc chloride (ZnCl2 ext{ZnCl}_2ZnCl2) or nitric acid (HNO3 ext{HNO}_3HNO3).
Mechanism: The polymerization takes place in a homogeneous liquid phase, yielding a viscous polymer dope directly at the end of the reaction vessel.
Advantages: Eliminates the intermediate step of dissolving dry polymer powder. The resulting "spinning dope" can often be piped directly to the spinning units, saving energy and processing time.
Disadvantages: Reaction kinetics are more complex, heat removal from highly viscous solutions requires sophisticated reactor design, and solvent recovery systems must be exceptionally efficient to handle large volumes of volatile organic liquids.
5. Controlling molecular weight and polydispersity
In both suspension and solution routes, controlling the molecular weight and molecular weight distribution (polydispersity index) is paramount for high-end fabrication.
Mechanical Strength: High molecular weights (MwM_wMw typically ranging from 100,000 to 300,000 g/mol) ensure that the entangled polymer chains possess sufficient tensile strength and elongation capabilities during drawing and spinning.
Chain Transfer Agents: To prevent the runaway growth of ultra-long chains that would make the spinning dope too viscous or gel-like, chain transfer agents (such as alkyl mercaptans) are carefully metered into the reaction mixture.
The molecular architecture established during these initial polymerization stages dictates the rheological behavior of the spinning dope, setting the stage for the intricate extrusion, coagulation, and washing phases that transform liquid polymer solutions into precursor filaments.
HTML
<!-- CONTINUATION OF HTML STRUCTURE: FIBER POST-PROCESSING, STABILIZATION, AND CARBONIZATION -->
<div class="article-section" id="washing-and-drawing">
3. Washing, purification, and Mechanical drawing
Once the polyacrylonitrile (PAN) dope has been extruded into filaments via wet or dry-jet wet spinning, the freshly formed coagulated fibers, often referred to as as-spun or gel fibers, contain significant amounts of residual solvent (such as dimethylformamide [DMF], dimethyl sulfoxide [DMSO], or aqueous sodium thiocyanate solutions) alongside remnants of coagulant baths. Removing these residues is critical not only for environmental and safety compliance but also for preventing microscopic voids and structural defects during subsequent high-temperature thermal treatments.
The nascent filaments are routed through a multi-stage washing line consisting of counter-current water baths maintained at progressively elevated temperatures. This gradual leaching ensures the efficient diffusion of residual solvent out of the polymer matrix without inducing osmotic shock, which can cause micro-cracking or surface blistering. Concurrently, the fibers undergo mechanical drawing, a crucial stretching process performed either while wet or immediately following washing. Plasticizing the polymer chains in a heated water or steam bath allows the rigid, tangled PAN macromolecules to disentangle and reorient themselves parallel to the fiber longitudinal axis. Achieving a high draw ratio (frequently between 4x and 10x, depending on the copolymer composition and molecular weight) maximizes molecular orientation and crystallinity, laying the foundation for high tensile strength and modulus in the final carbon fiber product.
</div>
<div class="article-section" id="stabilization-phase">
4. Thermal Stabilization (Pre-Oxidation)
The transformation of PAN precursor fibers into high-performance carbon fibers hinges on the stabilization phase, widely regarded as the most chemically complex and critical step in the entire fabrication sequence. Conducted in an oxidizing atmosphere (typically ambient air) at temperatures ranging from 200°C to 300°C, stabilization converts the thermoplastic linear PAN structure into a non-melting, thermally stable ladder polymer.
During this phase, several overlapping chemical reactions occur simultaneously:
Because stabilization reactions are strongly exothermic, precise temperature profiling and tension control are mandatory. The fibers must be kept under constant mechanical tension to prevent transverse shrinkage, which preserves molecular alignment and prevents filament fusion. The resulting stabilized fiber, often distinguished by its deep jet-black coloration, is now fully prepared for the extreme environments of carbonization.
</div>
<div class="article-section" id="carbonization-and-graphitization">
5. Carbonization and High-Temperature treatment
Following stabilization, the oxidized PAN fibers enter a carbonization furnace purged with an inert gas, such as nitrogen or argon, to prevent combustion. Carbonization is executed in distinct temperature zones ranging from 1,000°C to 1,500°C. As the temperature climbs, non-carbon elements, primarily hydrogen, nitrogen, oxygen, and residual volatile byproducts, are progressively driven off in the form of gases like water vapor, hydrogen cyanide, carbon monoxide, and ammonia.
As these heteroatoms depart, the remaining carbon atoms rearrange into turbostratic graphite ribbons oriented parallel to the fiber axis. The mass loss during this stage is substantial, often reducing the fiber weight by up to 50%, yet the overall physical volume and morphology remain remarkably intact due to the rigid network established during stabilization.
For applications demanding exceptionally high tensile modulus (stiffness), the carbonized fibers may undergo an optional graphitization step at temperatures soaring between 2,000°C and 3,000°C in an ultra-pure inert atmosphere. This secondary heat treatment promotes lateral growth of the graphene sheets and enhances structural perfection, though excessive temperatures can sometimes compromise ultimate tensile strength in favor of increased stiffness.
</div>
<div class="article-section" id="surface-treatment-and-sizing">
6. Surface treatment and sizing
Raw carbon fibers emerging from the carbonization or graphitization furnaces possess an inert, smooth, and chemically passive surface characterized by low wettability. If utilized directly in composite manufacturing, this passivity results in poor interfacial adhesion between the carbon reinforcement and matrix resins (such as epoxy, bismaleimide, or peek), leading to catastrophic delamination under shear stresses.
To rectify this, fibers pass through an electrolytic surface treatment bath, typically containing an acidic or alkaline aqueous electrolyte like ammonium bicarbonate or nitric acid. Controlled anodic oxidation introduces oxygen-containing functional groups (such as hydroxyl, carbonyl, and carboxyl groups) onto the fiber surface and creates micro-pits that increase the specific surface area and mechanical interlocking capability.
Immediately following surface activation, the fibers undergo sizing. A thin polymeric coating (sizing agent), compatible with target matrix resins, is applied via roller deposition and dried. Sizing serves dual purposes: it protects the brittle filaments from abrasive damage during handling, winding, and weaving, and it promotes optimal wetting and chemical bonding with composite resins during final component fabrication.
</div>
<div class="article-section" id="industrial-applications-outlook">
7. Conclusion and industrial outlook
The fabrication of polyacrylonitrile into advanced carbon fibers represents a masterclass in modern polymer engineering and materials science. From precise solution polymerization and specialized spinning technologies to multi-stage thermal processing and surface functionalization, every parameter dictates the mechanical performance of the resulting material.
Today, PAN-based carbon fibers form the structural backbone of numerous cutting-edge industries, including aerospace engineering (fuselages, wings, and propulsion components), high-performance automotive manufacturing, renewable energy (wind turbine blades), and sporting goods. Ongoing research focuses on developing bio-based or lower-cost acrylonitrile precursors, reducing energy consumption during stabilization, and optimizing inline processing speeds to meet expanding global demand for lightweight, high-strength composite materials.
</div>