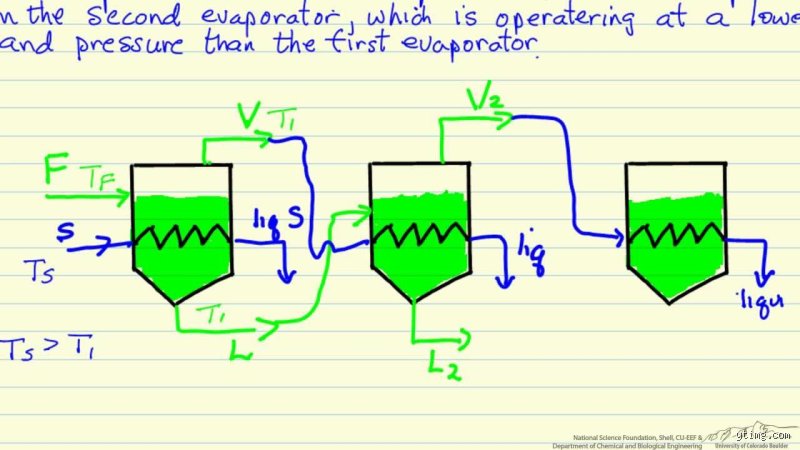
Boiling water requires an immense amount of latent heat. Historically, single-stage evaporation demanded fresh steam for every single kilogram of liquid vaporized, creating an economically unsustainable energy sink. Engineers recognized that vapor boiling off a solution still possessed valuable thermal energy rather than waste heat destined for cooling towers. Harnessing this secondary vapor to heat a subsequent vessel transformed the economics of concentration.
Thermodynamic cascading governs the entire mechanism. Steam enters the calandria of the first effect, transferring latent heat to boil the process liquor inside the tubes. This first vessel operates at the highest pressure and temperature within the battery. The vapor generated from the boiling liquor in the first effect then travels into the heating chest of the second effect. Because the second effect operates under a partial vacuum, its boiling point is significantly lower than that of the first vessel. Consequently, the vapor from the first effect acts as the heating medium for the second effect.
Repeating this energy recycling principle defines the third effect. Operating under an even deeper vacuum, the third vessel utilizes the vapor boiled off from the second effect as its primary heat source. Each successive vessel amplifies thermal efficiency, effectively wringing multiple duties out of a single initial injection of live steam.
Analyzing the internal pressure profile reveals why vacuum engineering remains critical to multi-effect systems. If pressures remained equal across all vessels, boiling point elevation would quickly halt heat transfer. By stepping down pressure—and consequently boiling temperature—from effect to effect, temperature differences are maintained across the heating surfaces without requiring excessively high temperatures in the initial stage. High initial temperatures can degrade heat-sensitive materials such as pharmaceutical compounds or delicate food juices like tomato paste or orange concentrate.
Comparing this cascading thermal architecture to a multi-tiered hydraulic gravity feed system illuminates the fluid dynamics at play. Just as water flows naturally down a terraced hillside from higher to lower elevations without mechanical pumping between each terrace, thermal energy cascades downward through decreasing temperature and pressure gradients. The vapor drives the phase change below it purely through differential pressure and latent heat release, requiring only pumps to transfer the liquid phase against the pressure gradient when operating in a forward-feed configuration.
Feed arrangement configurations profoundly impact performance characteristics. Forward-feed systems introduce the dilute feed liquor into the first, hottest effect and transfer it progressively to lower-pressure vessels. This configuration leverages natural pressure differentials to push liquid through the system without intermediate inter-effect pumps, simplifying mechanical design. Conversely, backward-feed arrangements pump cold, concentrated feed into the final low-pressure effect first, moving it sequentially toward the high-temperature steam chest. Each method presents distinct advantages depending on fluid viscosity, scaling tendencies, and thermal sensitivity.
Scaling and fouling present formidable operational challenges within multi-effect evaporators. As concentration increases across the sequence, dissolved minerals or organic compounds frequently reach saturation limits and precipitate onto heat transfer surfaces. Mineral scale acts as an insulating blanket, severely degrading heat transfer coefficients and forcing unscheduled shutdowns for chemical cleaning or mechanical descaling. Operators must carefully monitor fouling resistance factors and maintain optimal fluid velocities to mitigate boundary-layer stagnation.
Energy economy serves as the primary metric for evaluating multi-effect systems. An ideal single-effect evaporator achieves an economy of roughly 0.8 to 0.9 kilograms of water evaporated per kilogram of steam consumed. Expanding the setup to a three-effect configuration dramatically alters this equation, typically yielding an economy approaching 2.3 to 2.7 kilograms of water evaporated per kilogram of primary steam. This multiplication of thermal efficiency explains why industrial plants consuming thousands of tons of liquor daily view multi-effect concentration as an indispensable asset.
3. Operational flow configurations: Forward, backward, and mixed feed
The thermodynamic efficiency and mechanical longevity of a three-effect evaporator system depend heavily on how the process liquid (feed) is routed relative to the flow of heating steam. Engineers typically choose among three primary configurations based on the physical and chemical properties of the liquor being concentrated.
Forward feed (direct flow)
In a forward-feed configuration, both the raw feed and the heating steam enter the first effect in parallel.
Mechanism: The feed solution is pumped into Effect 1, where it is partially concentrated. The concentrated liquor is then transferred under pressure or vacuum differential to Effect 2, and subsequently to Effect 3.
Advantages: Because the solution is most dilute in the first effect (where temperatures are highest) and most concentrated in the final effect (where temperatures are lowest), problems related to high viscosity and crystallization are minimized at lower temperatures. No inter-stage pumps are typically required since pressure naturally decreases from Effect 1 to Effect 3.
Disadvantages: The incoming feed is usually at a temperature lower than the boiling point of Effect 1, requiring sensible heat input. Liquor viscosity increases significantly in the final effect, which can degrade the heat transfer coefficient where temperatures are already at their lowest.
Backward feed (Counter-Current flow)
In a backward-feed arrangement, the raw feed enters the final, coldest effect (Effect 3) and is pumped progressively backward through Effect 2 and finally into Effect 1.
Advantages: The concentrated, highly viscous liquor is subjected to the highest temperatures in Effect 1. High temperature dramatically reduces liquid viscosity, maintaining a high overall heat transfer coefficient (UUU) in the final stages of concentration. This setup is exceptionally efficient for liquids whose viscosity increases steeply with concentration.
Disadvantages: Inter-stage pumps are mandatory to force the fluid against the pressure gradient from low-pressure/low-temperature zones to high-pressure/high-temperature zones. Cold feed entering the final effect requires substantial preheating.
Parallel / mixed feed
Mixed feed configurations route different streams directly to intermediate effects or combine forward/backward flow characteristics to handle complex scaling behaviors, crystallization points, or specific thermal sensitivities of heat-sensitive pharmaceuticals and biological broths.
4. Quantitative performance metrics: Steam Economy and Heat Transfer
The primary engineering justification for employing a three-effect evaporator over a single-effect unit is steam economy, defined as the mass of water evaporated per unit mass of fresh steam supplied to the first effect.
Steam Economy=Total Mass of Vapor Evaporated (W1+W2+W3)Mass of Live Steam Consumed (S) ext{Steam Economy} = \frac{ ext{Total Mass of Vapor Evaporated ($W_1 + W_2 + W_3$)}}{ ext{Mass of Live Steam Consumed ($S$)}}Steam Economy=Mass of Live Steam Consumed (S)Total Mass of Vapor Evaporated (W1+W2+W3)
In an ideal single-effect evaporator, the steam economy is roughly 0.80.80.8 to 0.90.90.9. In a well-designed three-effect evaporator, the theoretical steam economy approaches 2.52.52.5 to 2.82.82.8, meaning nearly three kilograms of water are vaporized for every single kilogram of primary boiler steam consumed.
Critical engineering factors affecting performance
Boiling Point Elevation (BPE): As solute concentration increases, the vapor pressure of the solution drops, causing its boiling point to rise above that of pure water at the same pressure. This BPE effectively eats into the available temperature driving force (ΔT\Delta TΔT) across subsequent effects, necessitating larger heat transfer surface areas.
Hydrostatic Head Loss: The depth of liquid in the evaporator tubes creates a hydrostatic head that increases pressure at the bottom of the tubes, raising the local boiling point and reducing the effective temperature difference.
Overall Heat Transfer Coefficient (UUU): Ranging from scaling resistance on the tube walls to boundary layer thermal resistance, maintaining high UUU-values across all three effects dictates cleaning schedules and tube material selection (e.g., stainless steel, titanium, or graphite blocks).
5. Industrial applications across sectors
Three-effect evaporators are workhorses across heavy processing industries where massive volumes of solvent must be removed economically:
Sugar Refining: Concentrating clarified sugarcane or sugar beet juice from roughly 12-15% dissolved solids up to 65-70% heavy syrup prior to crystallization pans. Robert-type vertical tube evaporators are standard in this sector.
Chemical Processing & Salt Production: Concentrating brine solutions, caustic soda (NaOH ext{NaOH}NaOH), ammonium sulfate, and various inorganic salts before crystallization and centrifugation.
Pulp and Paper Industry: Concentrating black liquor derived from the Kraft pulping process to recover valuable cooking chemicals and generate high-pressure steam via recovery boilers.
Zero Liquid Discharge (ZLD) & Wastewater Treatment: Reducing industrial effluent volumes, treating desalination reject streams, and concentrating high-TDS (total dissolved solids) wastewater prior to solidification.
6. Operational challenges, Scaling, and mitigation
While highly efficient, operating a three-effect system introduces unique engineering headaches that require rigorous monitoring and preventive maintenance:
Fouling and Scaling: Dissolved minerals (such as calcium sulfate, silica, or calcium carbonate) precipitate onto heating surfaces as solubility limits are exceeded during concentration. This thermal insulation layer drastically reduces heat transfer coefficients.
Corrosion and Stress Corrosion Cracking: High operating temperatures coupled with aggressive chemical environments (e.g., concentrated chlorides or caustic solutions) mandate precise metallurgical selection.
Foaming: Organic impurities can cause severe foaming, leading to liquid carryover into vapor lines (entrainment). Engineers install centrifugal mist eliminators or demisters between effects to protect downstream condensers and vacuum systems.
7. Modern innovations: VVR, MVR, and automation
Recent advancements have pushed the boundaries of traditional multi-effect evaporation efficiency:
Thermal Vapor Recompression (TVR): By utilizing a high-pressure steam ejector to draw a portion of secondary vapor from an earlier or intermediate effect and re-mix it with live steam, plant operators boost the effective thermal head and improve steam economy without adding another full effect vessel.
Advanced Process Control: Modern facilities employ distributed control systems (DCS) integrated with real-time density meters, online viscometers, and automated condensate purging loops to stabilize boiling regimes and optimize energy consumption dynamically.
Conclusion
The three-effect evaporator represents a masterclass in applied thermodynamics and chemical engineering design. By artfully cascading latent heat across three interconnected pressure stages, these systems achieve an optimal balance between capital expenditure (equipment cost) and operational expenditure (energy consumption). Whether sweetening the global food supply in sugar mills or treating complex industrial effluents for environmental compliance, the triple-effect configuration remains an enduring cornerstone of modern industrial separation technology.